

Turn contaminated sulphur into pure sulphur.
Modular, steam-heated remelters that recover wet, sandy, rocky and reclaimed sulphur to 99.5% purity, ready to sell. Custom-designed for every application.
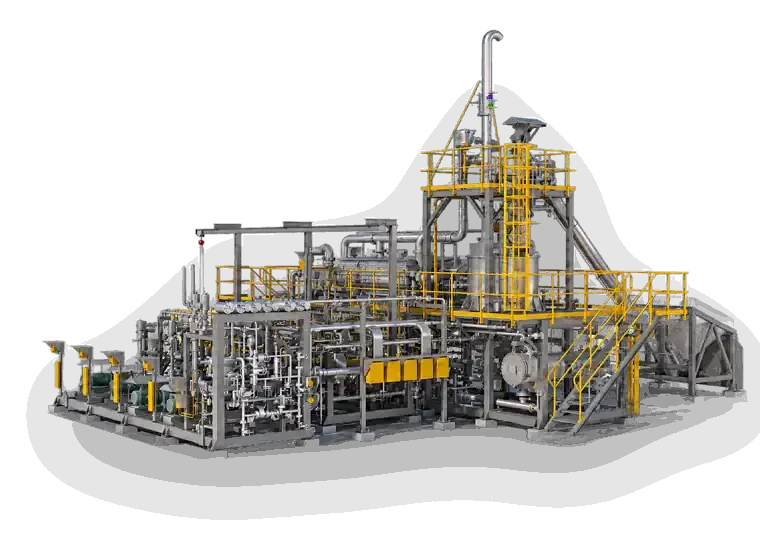
Contaminated sulphur is a cost. It doesn’t have to be.
Every sulphur plant accumulates it: spillage around conveyors and loaders, carryover from forming units, old block and base-pad material, off-spec product that sits in the yard for years.
Remelting it properly takes more than a heated pit: water flashes and foams, and sand and rock settle where they shouldn’t. Our remelters are designed around that reality by people who have operated sulphur plants, not just drawn them.
The result: contaminated sulphur goes in, pure 99.5% sulphur comes out, ready to go back to molten storage and be formed and sold.
Without a remelter, owners are left with
- Landfill costs — paying to dispose of a product that should be sold.
- Contaminated pits — dirty feed returned to molten storage fouls tanks, pumps and forming units.
- Growing stockpiles — dust, run-off and environmental exposure every season.
- Open-pit melting — emissions, splashing and foaming hazards for operators.
Four stages, one continuous process
Every system is custom-designed to the client’s feed composition and throughput. Process scheme shown for the ADNOC Ruwais configuration.
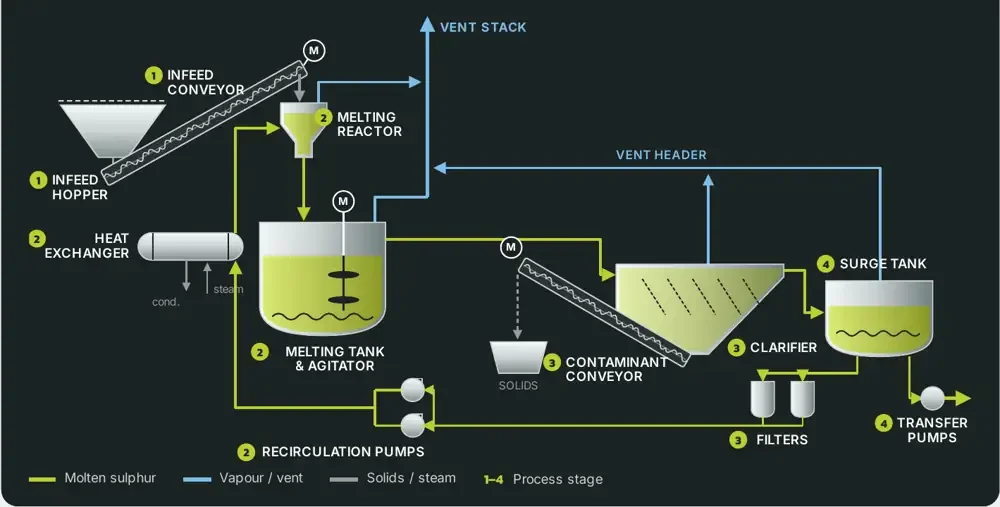
Feed
A grizzly-screened hopper rejects oversize lumps; the infeed screw conveyor meters solid sulphur into the melting reactor.
Melt
Feed meets hot recirculated sulphur (135–145 °C) in the jacketed reactor, flashing off most moisture. The agitated tank completes melting; recirculation pumps and the heat exchanger keep the loop hot.
Clean
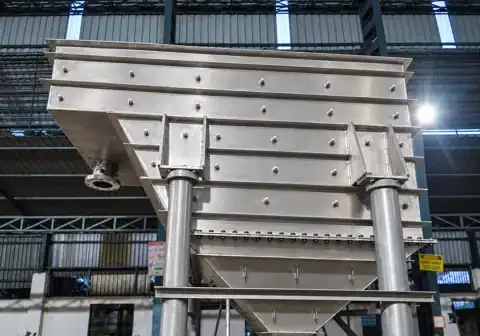
Melt overflows into the heated clarifier; sand and rock settle on inclined plates and the contaminant conveyor lifts them out. Filters polish the recirculating sulphur.
Deliver
Clean sulphur overflows to the coil-heated surge tank and transfer pumps return it to molten storage.
Engineered around the feed, not a catalogue.
Feedstock changes from site to site and stockpile to stockpile, so every Safe Sulphur remelter starts from a feed analysis (moisture, sand, rock, ash, acidity) and scales from 10 to 500 t/d. Each design makes sure contamination leaves the process instead of building up inside it.
Handles wet, sandy, rocky feed
Designed for reclaimed block, spillage and forming carryover containing water, rock and sand.
Contaminants leave the process
Inclined-plate clarifier and contaminant conveyor for continuous solids removal, backed by duplex filters on both loops.
Modular skids, less site work
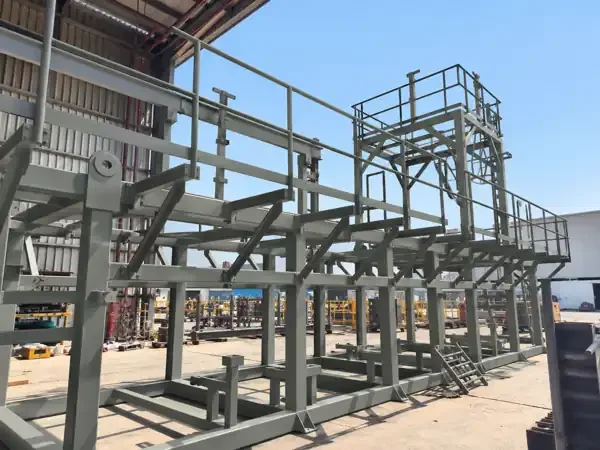
Pre-piped, pre-wired skids, factory tested before shipment and set on prepared foundations.
Hazardous-area rated
Instruments and electrical equipment certified Ex for both gas and combustible-dust zones.
All-steam heating
Steam-jacketed piping and equipment, steam tracing and a steam heat exchanger, with no electric heat tracing.
Delivered to owner standards
Engineered and documented to national-oil-company specifications.
From a single skid to a full reclaim system
Compact skid
For granulated or clean crushed sulphur. Melting tank, agitator, filters and pumps on one skid, with cable trays and piping to a single tie-in point.
Contaminated-feed system
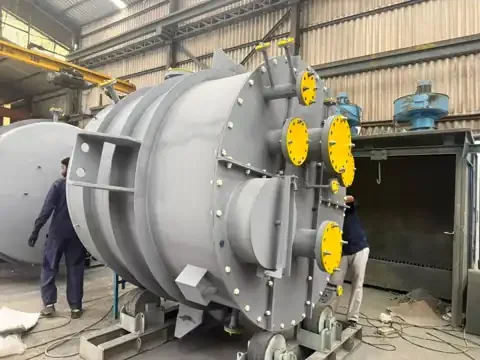
Adds the melting reactor, clarifier, contaminant conveyor, surge tank and heat exchanger for reclaimed and spill material, as supplied to ADNOC.
Custom & integrated
Block reclamation and remelt, pit upgrades or integration with forming plants, from feasibility study and FEED through supply.
Typical design basis
| Capacity | Scalable from 10 to 500 t/d |
| Design | Custom-designed for every application, based on the feed composition |
| Feed | Granulated, crushed-block or reclaimed solid sulphur, including material contaminated with water, sand and rock |
| Product | Molten sulphur recovered to 99.5% purity, returned to storage for forming |
| Heating | Low-pressure steam: jacketed piping and equipment plus a heat exchanger |
| Area class. | Ex-certified instruments and motors for gas and dust zones |
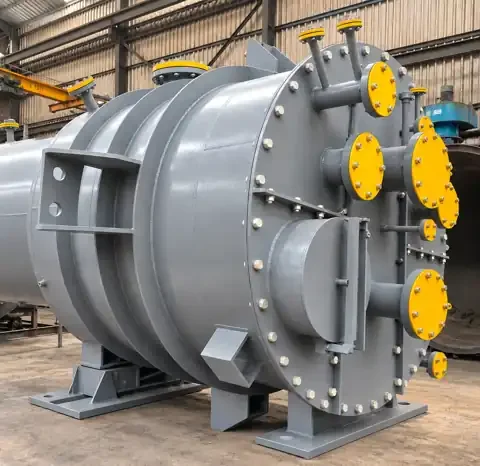
| Construction | Stainless steel tanks, heat exchanger, infeed hopper, screw conveyor and vent line; carbon steel skid frames with platforms and access |
| Controls | Local control stations and field instruments, ready to interface with the plant DCS |
| Testing | FAT at our UAE assembly facility; SAT and commissioning support on site |
Feedstock composition varies, so every unit is custom-designed. Figures are typical and confirmed against the client’s feed analysis.
ADNOC Ruwais contaminated sulphur remelter
Solid sulphur had built up at Ruwais contaminated with water, rock and sand from process carryover and handling spillage. Earlier designs by other providers left two poor options: landfill it, or feed it to the sulphur pits and contaminate those too.
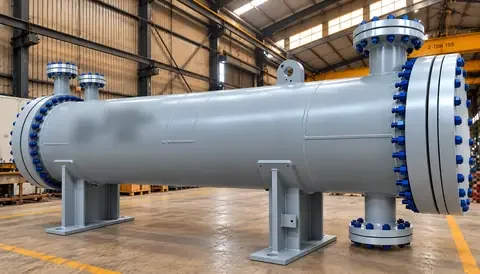
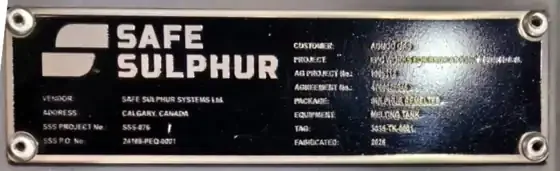
Safe Sulphur custom-designed a three-skid remelting package to recover that material to 99.5% purity and return it to the molten sulphur tank for re-granulation. The package is scheduled to enter service in 2026.

One team from feed sample to first molten sulphur
Assess
Site audit and feed analysis to set capacity, contamination and utilities.
Engineer
In-house process, mechanical, piping, structural, E&I and civil design.
Fabricate
Qualified vessel shops with Western OEM pumps, agitators and instruments.
Assemble & test
Skid assembly and FAT at Safe Sulphur Emdad LLC, Abu Dhabi.
Commission
Site assembly guidance, SAT, start-up and operator support.
Remelting track record
Send us your feed analysis and target throughput.
We’ll come back with a concept and budget price. Canadian sulphur specialists since 2003, with UAE assembly for faster delivery across the Gulf.
info@safesulphur.com
Safe Sulphur Systems Ltd. · Calgary, Canada
Safe Sulphur Emdad LLC · Abu Dhabi, UAE
What to send us
- Feed type: granulated, crushed block, reclaimed or spill
- Target throughput (t/d)
- Contamination: moisture, sand, rock, ash, acidity
- Site location and available utilities